
 English

Sealless Does Not Mean Maintenance-Free
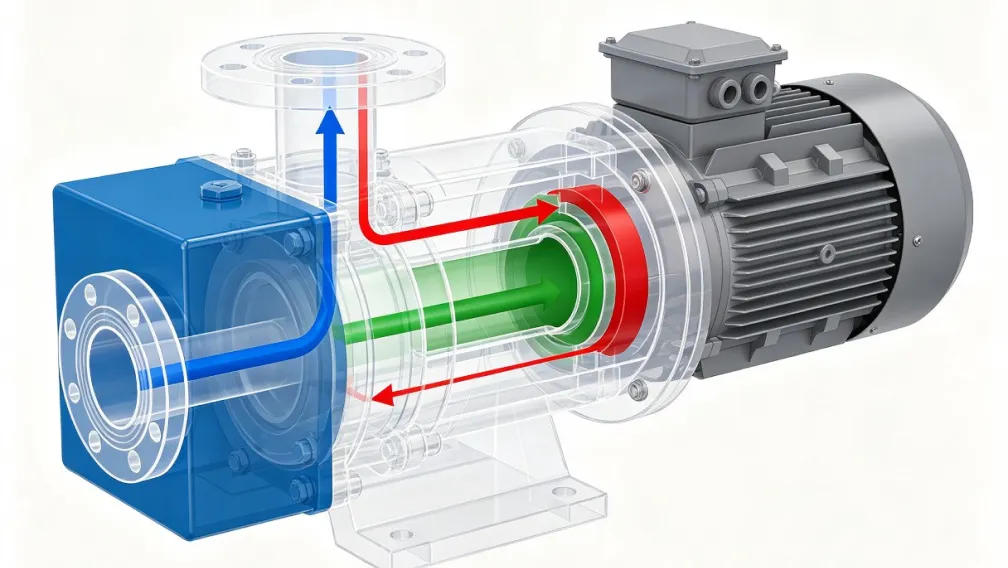
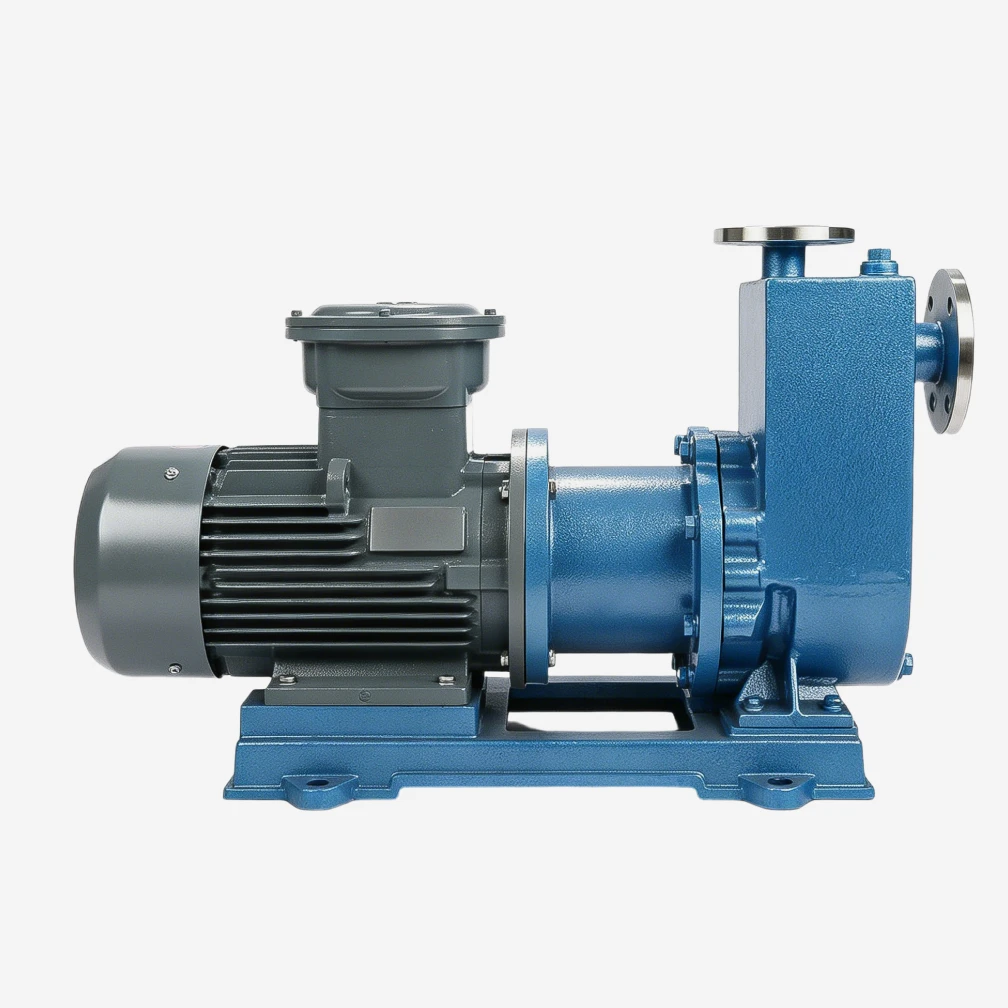
A magnetic drive pump removes the mechanical seal, and with it the single highest-maintenance component of a conventional chemical pump. What remains is a different set of wearing parts: internal sleeve bearings lubricated by the pumped liquid, a containment shell that holds the pressure boundary, and a magnetic coupling with a finite torque rating. These components fail rarely, but when they do, they fail fast and with little external warning. Magnetic drive pump maintenance is therefore a discipline of monitoring conditions rather than adjusting hardware: keep the pump wet, keep the internal circulation clean, respect the torque limit, and inspect the internal parts on a planned interval before their failure finds the casing. This guide covers the working discipline and the inspection scope for sealless chemical pumps.
Keep It Wet: The Dry-Running Rule
The internal sleeve bearings of a magnetic drive pump, commonly silicon carbide, are lubricated and cooled by the pumped liquid itself, and the containment shell depends on the same internal circulation to carry away heat. Without liquid, friction heat has nowhere to go, and bearings and shell can be scorched within seconds. This makes dry running the single most destructive event in a sealless pump's life, and preventing it is an operational system, not an instruction on a sticker.
Three protections cover the realistic dry-running scenarios. First, verify prime before every start: the pump must be vented and confirmed full of liquid, including after any maintenance that drained the casing. Second, protect against suction loss during operation. A power monitor that trips the motor when power draw falls below the no-flow threshold is the standard instrument, because a pump that has lost suction unloads immediately and the power drop arrives before the damage. Third, control the discharge side: running against a closed or blocked discharge stops internal circulation just as surely as losing suction, so minimum-flow requirements apply to sealless pumps without exception.
Sleeve Bearing Care
What Wears the Bearings
Silicon carbide sleeve bearings tolerate corrosive chemistry almost indefinitely; what wears them is mechanical. Abrasive particles carried into the bearing housing grind the running surfaces, and because the internal circulation feeds the bearings directly from the process fluid, fluid cleanliness is a bearing life factor. Ferrous debris is a special case: it is drawn into the magnetic field between the rotors and accumulates in the gap, accelerating wear from the inside. An inlet strainer on dirty services, cleaned on schedule, is cheap insurance. The second wear driver is hydraulic: sustained operation far from the best efficiency point raises radial loads on the internal bearings, so duty-point reviews belong in sealless maintenance just as they do in sealed-pump maintenance.
Measuring Bearing Condition
Bearing condition is assessed by clearance. During a planned outage, measure shaft radial play at the impeller end and compare it against the manufacturer's limits. Excessive play means the sleeve bearings are worn, and the correct response is replacement before the wear progresses: an impeller running on worn bearings eventually contacts the casing lining, converting a bearing kit into a casing repair. Record every clearance measurement in the pump's history file; the wear rate between overhauls is the data that justifies extending or shortening the inspection interval for that specific duty.
Containment Shell Care
The containment shell is the pressure boundary that makes the pump sealless, and its failure converts a zero-leakage pump into an uncontained one. Three damage mechanisms account for nearly all shell failures. Thermal damage comes first: heat from dry running or from a stalled internal circulation scorches and distorts non-metallic shells, and on metallic shells eddy-current heating rises sharply when the pump runs unloaded or handles fluids outside its design conductivity range. The weekly check is simple: inspect the shell area for heat discoloration, which is the visible record of a thermal event. Mechanical damage follows: a worn bearing that lets the inner rotor contact the shell scores it from inside, which is why bearing clearance and shell inspection belong in the same outage. Chemical attack is the third: verify at specification that the shell material, metallic or non-metallic, is compatible with the actual fluid, and at inspection look for swelling, cracking, or crazing that signals incompatibility developing over time.
Decoupling: Response and Consequences
When impeller load exceeds the magnetic coupling's torque rating, the inner and outer rotors slip: the motor keeps running, the impeller stops, and flow ceases. The usual causes are a viscosity rise, a blocked discharge line, solids jamming the impeller, or a startup against an unexpectedly dense fluid. The response procedure matters. Shut down immediately, because a decoupled coupling is generating heat in the shell with no useful work coming out. Let the magnets cool, identify and clear the overload cause, then restart. Do not simply re-energize a decoupled pump and hope: repeated decoupling events permanently demagnetize the coupling, progressively lowering its torque ceiling until the pump can no longer carry its rated duty. A pump that has decoupled repeatedly needs a coupling torque check at its next overhaul, not just a restart.
The External Discipline
Much of sealless maintenance is conventional pump discipline applied to a machine that punishes lapses faster. Alignment still matters: the motor and pump shafts carry the coupling magnets, and misalignment loads the internal bearings. Instrumentation still matters: discharge pressure and motor amperage trends catch impeller wear and developing blockages exactly as they do on sealed pumps. And temperature monitoring matters more: bearing housing temperature on a sealless pump is one of the few external windows into internal condition, and a slow upward trend is worth an inspection even when every other reading looks normal. Vibration monitoring applies too, with the caveat that internal bearing wear in a sealless pump often shows as a subtle broadband rise rather than the classic bearing tones.
Maintenance Schedule for Sealless Pumps
| Interval | Task |
|---|---|
| Daily | Confirm flow and pressure in normal band; check shell area temperature; listen for abnormal noise |
| Weekly | Inspect shell area for heat discoloration; verify power monitor trip function; check strainer differential on dirty services |
| Monthly | Review duty point and amperage trend; alignment check; temperature trend review |
| Quarterly | Visual containment shell inspection; bearing clearance spot check where design permits |
| Annual | Replace sleeve bearings; inspect shell for scoring, swelling, and cracking; coupling torque and magnet condition check; measure and record all clearances |
What Sealless Maintenance Eliminates, and What It Demands in Spares
The maintenance case for sealless pumps rests on what disappears from the schedule. There is no flush plan to verify weekly, no barrier fluid to pressure, sample, and cool, no seal faces to trend and replace, and no seal-related leakage to log. For plants running dozens of sealed pumps, moving the worst services to magnetic drive removes a disproportionate share of the maintenance hours, because seal work dominates sealed-pump labor.
The spares strategy changes shape accordingly. A sealed pump's shelf holds seal face sets and elastomers; a sealless pump's shelf should hold a complete set of sleeve bearings, a spare containment shell, and the internal O-rings for the wetted end. Bearing kits are consumables with a predictable annual replacement rhythm, so stock them by population. The containment shell is different: it should never wear in normal service, but its replacement involves the pressure boundary of a hazardous-fluid pump, and lead times can be long. One spare shell per pump model in critical service converts a potential month of downtime into a single outage. Coupling magnet assemblies rarely need replacement, but a pump with a history of decoupling events should carry one, because a weakened coupling only reveals itself under load.
Conclusion
A magnetic drive pump trades seal maintenance for a stricter operational discipline: never run it dry, keep the process fluid that feeds its bearings clean, respect the coupling's torque limit, and open it on plan to measure bearings and shell before wear finds the pressure boundary. Managed this way, sealless pumps routinely run for years between overhauls with nothing but external checks. YFTEL supplies sleeve bearing kits, containment shells, and coupling assemblies for the full CQB magnetic drive pump range, alongside the sealed centrifugal chemical pumps that share the same installation discipline. Send us your duty conditions and maintenance history, and our engineers will help you set inspection intervals that match your actual wear rates.
-

YFTEL Pumps
Fluid Engineers & Technical Support, YFTEL Pump
YFTEL is a chemical pump manufacturer based in Hangzhou, China, with a 26,000 m² production base in Hangzhou, China, with a 26,000 m² production base in Anhui. Using the CAS-patented Fluoroplastic Alloy material, we produce 300+ models of corrosion-resistant pumps, valves and piping, exported to 30+ countries.