
 English

The Engineering Reality of Chemical Fluid Transfer
In standard municipal water systems, corrosion is a gradual process measured in decades, usually manageable through basic preventative maintenance. In industrial chemical processing, however, corrosion is an immediate, aggressive, and continuous threat. Transferring concentrated mineral acids, active halogens, heated organic solvents, and abrasive chemical slurries subjects fluid transfer equipment to extreme metallurgical stress. In these environments, corrosion in a pump is not merely a cosmetic issue—it is a fundamental failure of the pressure boundary that directly threatens plant safety, operational uptime, and the Total Cost of Ownership (TCO). Understanding why corrosion resistance matters requires a technical analysis of how specific components fail under chemical attack and the cascading operational consequences of those failures.
The Mechanics of Component Degradation
A centrifugal pump operates as a precise hydraulic machine. Its ability to maintain pressure, transfer kinetic energy, and seal hazardous fluids relies entirely on strict dimensional tolerances. When the wetted material is chemically incompatible with the process fluid, these tolerances are rapidly destroyed.
Casing Thinning and Pressure Containment Failure
The pump casing (volute) acts as a pressure vessel. Industrial process pumps routinely operate at internal system pressures ranging from 1.0 MPa to 1.6 MPa, with large pipeline systems exceeding 2.5 MPa. When corrosive fluids attack a metallic casing, uniform corrosion occurs, steadily dissolving the inner wall and reducing the material thickness. As the casing thins, its tensile strength decreases. Operating a thinned, corroded pump casing under high system pressure introduces a critical risk of catastrophic rupture. A ruptured casing immediately releases massive volumes of toxic or highly pressurized fluid into the plant environment, presenting a severe occupational hazard and triggering immediate environmental reporting protocols.
Impeller Erosion and Loss of Hydraulic Efficiency
The impeller is the kinetic heart of the pump, engineered with precise blade geometries designed via computational fluid dynamics (CFD). When exposed to strong acids or combined erosion-corrosion (chemical attack accelerated by abrasive particles), the edges of the impeller blades dissolve and pit. This degradation causes the pump to slip off its Best Efficiency Point (BEP).
As hydraulic performance degrades, the pump must draw more electrical current to achieve the same flow rate, massively inflating energy costs. Furthermore, asymmetrical corrosion on the impeller creates severe rotational imbalance. At speeds of 2900 r/min, this imbalance generates heavy radial vibrations that destroy the pump bearings and shatter the mechanical seal faces within days.
Shaft Pitting and Mechanical Seal Destruction
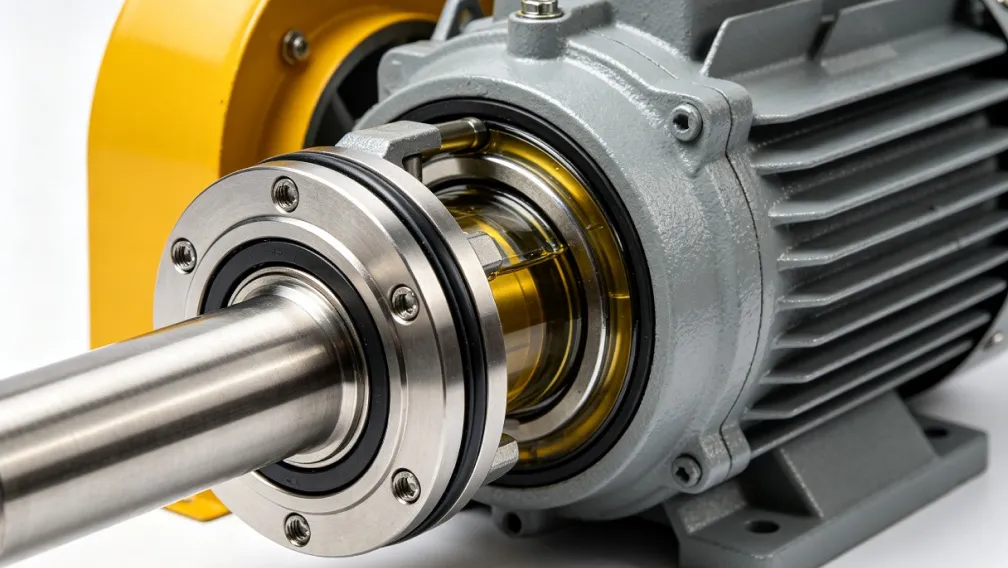
The dynamic mechanical seal prevents high-pressure fluid from escaping along the rotating pump shaft. The integrity of this seal depends on the shaft remaining perfectly smooth and concentric. If corrosive fluid migrates into the seal chamber and attacks a standard metallic shaft, pitting corrosion occurs. These microscopic pits act as a grinding file against the seal’s elastomers and O-rings, tearing them apart. Additionally, corrosive fluids will dissolve the metallic compression springs that hold the seal faces together. Once spring tension is lost, the seal opens, resulting in continuous, hazardous chemical leakage. This specific vulnerability is the primary driver of chronic centrifugal pump problems and solutions across heavy industry.
The Operational Consequences of Substandard Materials
Specifying a pump constructed from materials that are only "marginally" compatible with the process chemical is a frequent engineering error driven by initial capital cost reductions. However, the operational consequences of this compromise vastly outweigh the initial savings.
Catastrophic Safety Hazards
The leakage of toxic, highly flammable, or strongly acidic liquids directly endangers personnel. A spray of concentrated sulfuric acid or volatile benzene from a failed mechanical seal can cause severe injury, ignite in explosive atmospheres, and cause massive structural damage to the surrounding plant concrete and infrastructure. Reliable process pump solutions must guarantee environmental containment to comply with stringent EPA and ISO safety mandates.
Unplanned Downtime and Production Halts
Industrial facilities, such as chlor-alkali plants, petrochemical refineries, and continuous steel pickling lines, operate 24 hours a day. The failure of a single chemical transfer pump halts the entire production sequence. The true cost of a corroded pump is not the price of a replacement impeller; it is the tens of thousands of dollars lost per hour in stalled production. Relying on highly corrosion-resistant materials ensures continuous, uninterrupted operational uptime.
Product Contamination and Ionic Leaching
When acids attack standard metallic pumps (like cast iron or 304 stainless steel), the metal ions—such as iron, nickel, and chromium—dissolve directly into the process fluid. In sectors like pharmaceutical API synthesis, food processing, and fine electroplating, introducing trace heavy metals into the fluid stream will instantly spoil the batch. A contaminated batch of semiconductor-grade chemicals or pharmaceutical intermediates results in massive financial write-offs. Absolute chemical inertness is required to protect the purity of the final product.
Rising Maintenance and Lifecycle Costs
A pump suffering from chemical attack demands constant attention. Frequent replacement of mechanical seals, emergency bearing replacements, and labor costs for extracting and rebuilding the pump compound the operational expenditure (OPEX). Selecting an intrinsically corrosion-resistant pump architecture dramatically reduces the frequency of maintenance interventions, lowering the Total Cost of Ownership (TCO) over the equipment's lifecycle.
Formulating Reliable Industrial Pump Solutions
Because the consequences of corrosion are so severe, modern chemical pump engineering has shifted away from relying solely on expensive, exotic metallic alloys (like Hastelloy or Titanium) toward advanced composite polymers and magnetic drive architectures.
The Fluoroplastic Lined Concept
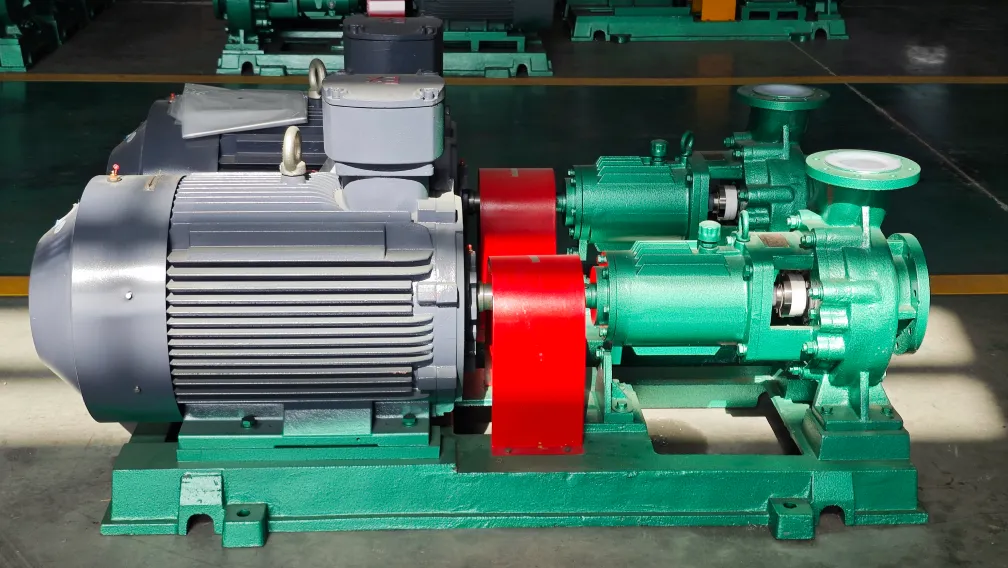
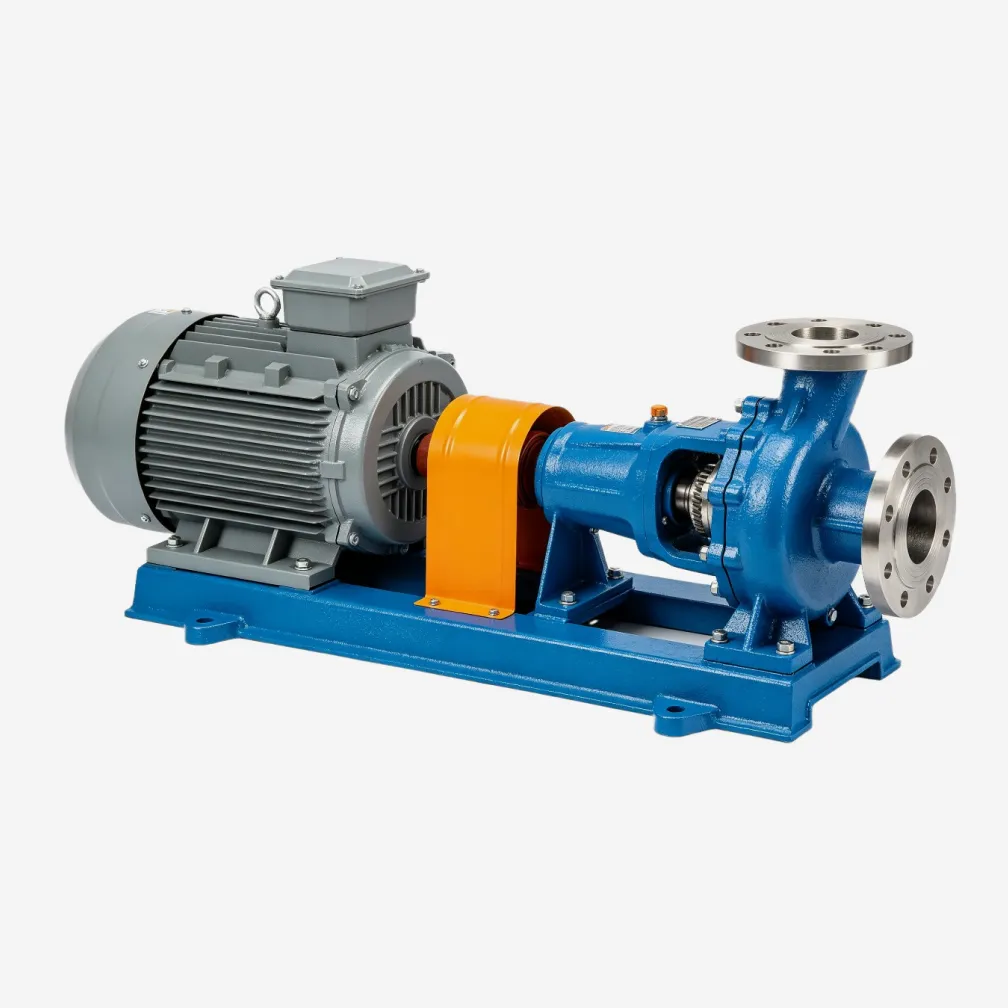
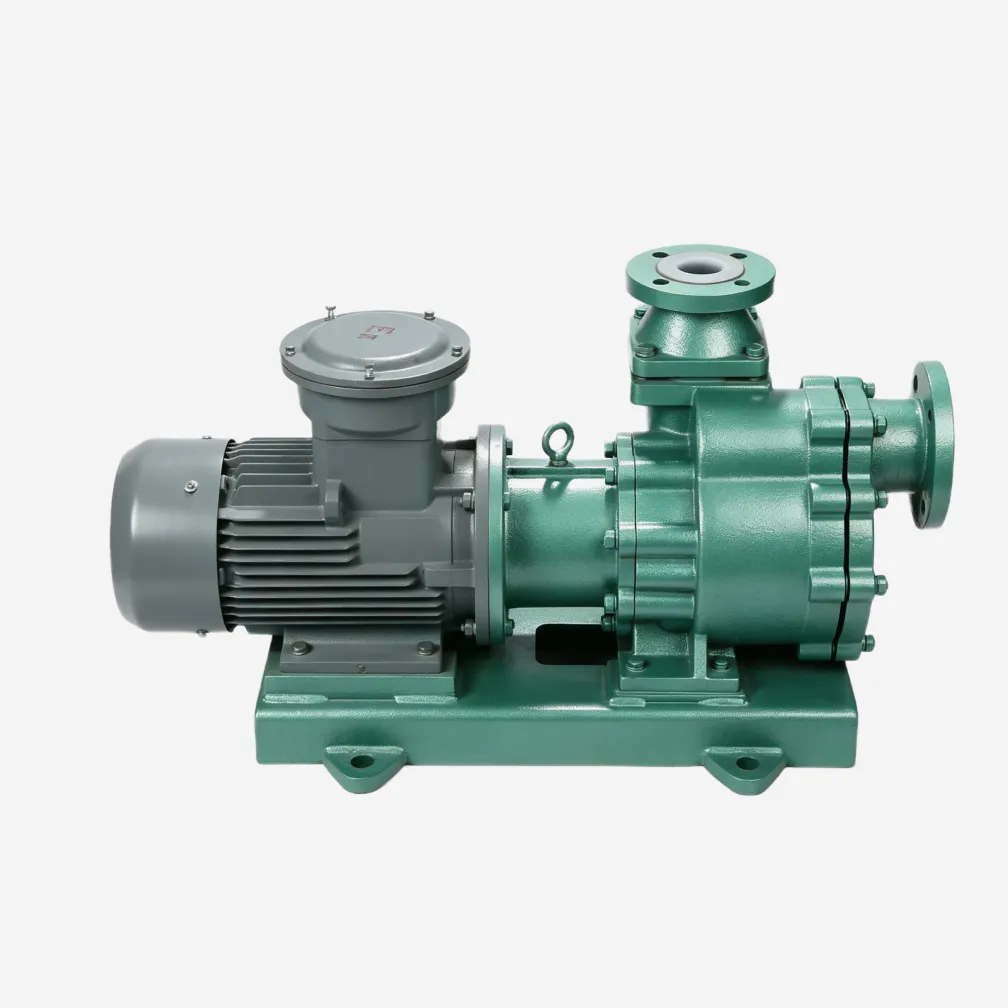
The most effective method to combat uniform and localized corrosion is to prevent the chemical from ever contacting metal. This is achieved through fluoroplastic-lined metal housings. In heavy-duty units like the IHF centrifugal pump, a robust cast iron or steel outer shell provides the necessary mechanical strength and pressure containment. The entire internal cavity is thickly lined with F46 (Perfluoroethylene propylene) or PTFE.
This design isolates mechanical load-bearing from chemical resistance. The fluoroplastic carries the corrosion burden, providing near-universal resistance to acids, alkalis, and strong oxidizers at temperatures up to 150°C. Because the lining is continuous, there is zero galvanic interaction and zero metal ion leaching, ensuring product purity and structural safety.
Handling Corrosive and Abrasive Slurries
When the fluid stream contains hard crystalline solids or ore pulps alongside corrosive acids (such as in wet metallurgy or phosphate fertilizer plants), standard fluoroplastics can suffer from mechanical scratching. The specialized solution here is the UHB-ZK slurry pump. It replaces the fluoroplastic with an 8 to 20 mm thick layer of Ultra-High-Molecular-Weight Polyethylene (UHMWPE). UHMWPE combines excellent acid resistance with a phenomenally low coefficient of friction, absorbing the impact of abrasive particles and outlasting hardened cast iron in severe slurry duties.
Achieving Zero-Leakage with Magnetic Drives
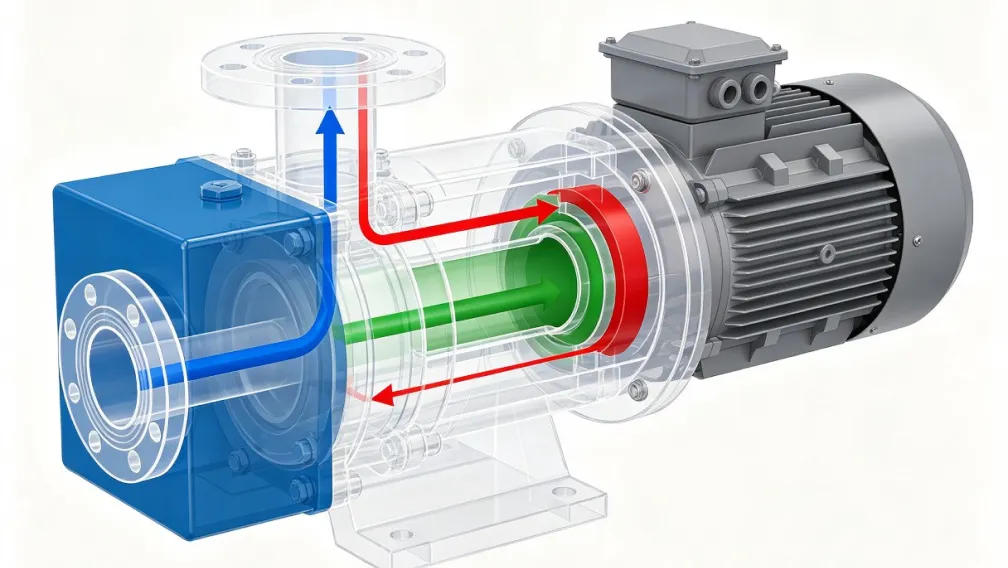
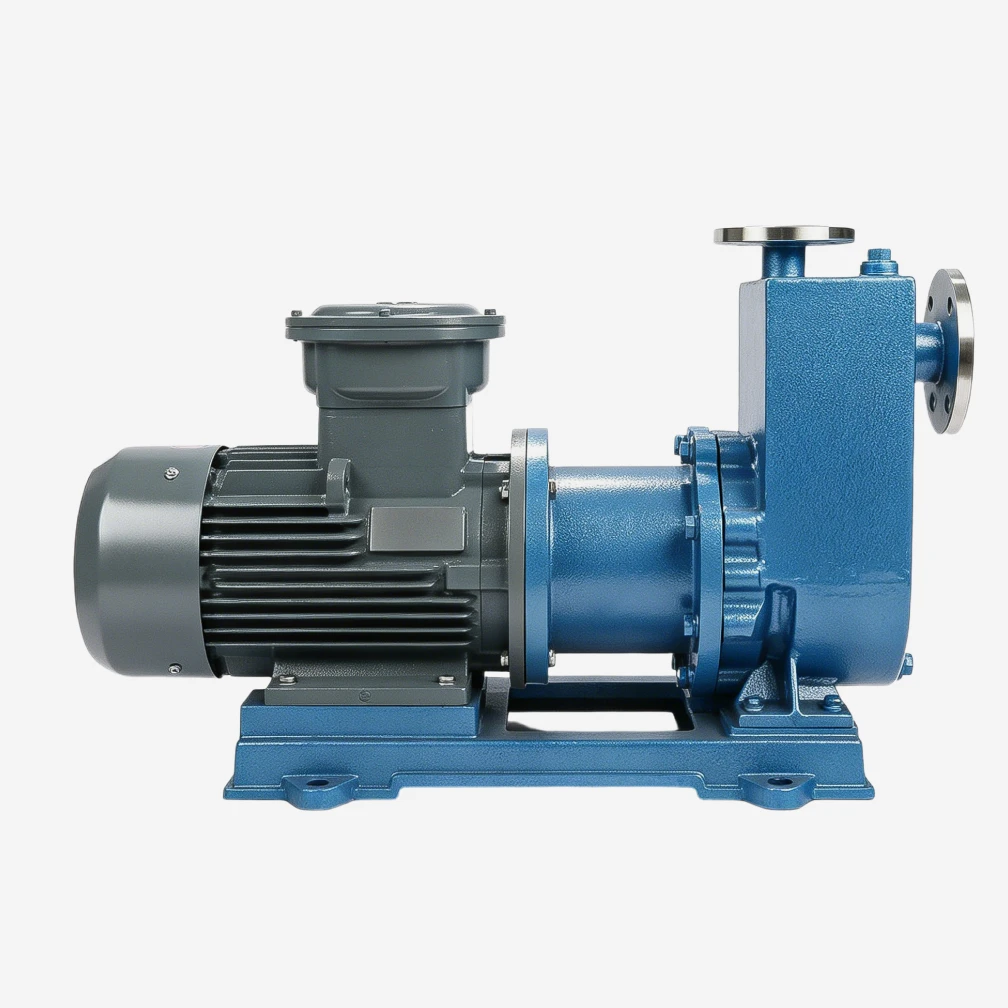
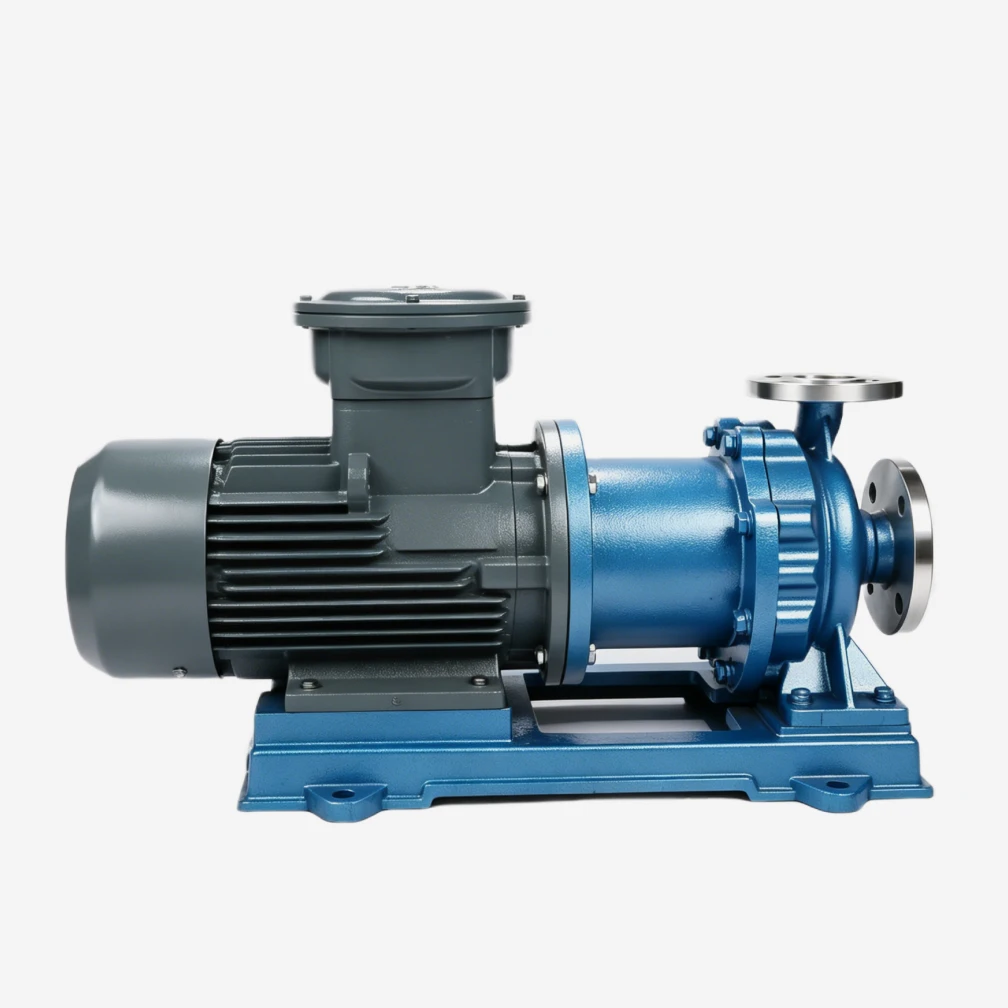
To definitively solve the issue of corrosive fluids destroying dynamic mechanical seals, engineers deploy sealless magnetic drive technology. In pumps such as the CQB magnetic drive pump, the physical shaft penetration is completely eliminated. A stationary non-metallic isolation sleeve hermetically seals the corrosive fluid inside the casing. Motor torque is transmitted via a magnetic field. By utilizing a static containment boundary and internal Silicon Carbide (SiC) bearings, these pumps provide absolute zero-leakage performance, ensuring maximum safety when transferring highly toxic, volatile, or precious corrosive liquids.
Conclusion: The Value of Precision Material Selection
Selecting a material that is chemically compatible with the pumped medium—and a construction architecture that prevents dynamic leakage—is the single most important decision in chemical pump specification. Failing to prioritize corrosion resistance guarantees elevated maintenance costs, unexpected downtime, and severe safety risks. When engineering a new fluid transfer loop or replacing failing equipment, prioritize absolute chemical compatibility. Provide your specialized pump manufacturer with precise data—including fluid composition, concentration, specific gravity, and operating temperature—to secure a pumping solution that ensures decades of safe, uninterrupted service.
-

YFTEL Pumps
Fluid Engineers & Technical Support, YFTEL Pump
YFTEL is a chemical pump manufacturer based in Hangzhou, China, with a 26,000 m² production base in Hangzhou, China, with a 26,000 m² production base in Anhui. Using the CAS-patented Fluoroplastic Alloy material, we produce 300+ models of corrosion-resistant pumps, valves and piping, exported to 30+ countries.