
 English

Corrosion Is the Primary Design Constraint in Chemical Pumping
In most pump applications, the specification starts with flow and head. In chemical service, it starts with a different question: will the pump survive the fluid? Corrosion resistance matters because it defines whether a pump is a long-term asset or a recurring failure. A pump that moves corrosive fluid efficiently for three months and then leaks is not a cheap pump; it is an expensive one with unpaid bills in downtime, lost product, safety exposure, and replacement labor. This article explains the specific corrosion mechanisms that attack pumps, what corrosion actually costs an operating plant, and how corrosion resistance is engineered into modern chemical pump design.
The Corrosion Mechanisms That Attack Pump Components
Corrosion inside a pump is rarely one process. Several mechanisms act at once, and each one targets a different component.
Uniform Attack on Casings and Covers
Uniform corrosion dissolves the wetted surface at a roughly even rate. On a cast iron or carbon steel casing carrying hydrochloric acid, wall thickness can fall by several millimeters per year. Because the casing is the pressure boundary, thinning directly reduces the maximum safe working pressure. The failure mode is a rupture under system pressure, not a drip.
Pitting and Crevice Corrosion at Stagnant Zones
Stainless steels resist uniform attack in many media but remain vulnerable to localized attack in chloride-bearing fluids. Pitting concentrates at surface defects and produces deep, narrow holes that penetrate a wall while the surrounding metal looks sound. Crevice corrosion does the same work under gaskets, O-ring seats, and deposit layers, exactly the geometries a pump is full of. A pump can pass a visual inspection and still be days from perforation.
Galvanic Corrosion Between Dissimilar Metals
When two different metals share a wetted path in an electrolyte, the less noble metal corrodes preferentially. A stainless shaft running in a cast iron casing, or a bronze impeller on a steel shaft, creates a galvanic couple that consumes one component to protect the other. Mixed-metal construction in corrosive service fails from the inside out, often at the component that was assumed to be the strongest.
Erosion-Corrosion at High-Velocity Surfaces
Impeller vanes, volute cutwaters, and seal faces see the highest fluid velocities in the machine. Here, mechanical stripping of the protective surface film combines with chemical attack, and the combined rate exceeds the sum of the two acting alone. Add suspended solids, as in hydrometallurgical leach streams or phosphate slurries, and erosion-corrosion can consume an unprotected impeller in weeks. This is the reason corrosive slurry service uses thick UHMWPE-lined slurry pumps rather than thin-lined or metallic designs.
What Corrosion Actually Costs a Plant
The purchase price of a pump is a small fraction of its lifetime cost. Corrosion attacks the budget through four channels, and each one dwarfs the initial saving from under-specifying materials.
Unplanned Downtime
A corroded pump fails on its own schedule, usually at full production. In continuous processes such as chlor-alkali, pickling lines, or PCB etching, one pump stopping can force an entire line down. Restarting a chemical line involves draining, neutralizing, and re-qualifying product, so the true downtime cost is measured in shifts, not hours.
Energy Waste from Degraded Hydraulics
Corrosion roughens flow passages and blunts impeller vanes. The pump drifts away from its best efficiency point and draws more power to deliver the same duty. Industry studies consistently identify pumping as one of the largest electrical loads in process plants, and a corroded impeller silently inflates that load every hour it runs. The wasted energy over a single year can exceed the price of a correctly specified replacement.
Safety and Environmental Exposure
Corrosion is the leading mechanical cause of containment loss in chemical transfer equipment. A seal face etched by pitting, or a casing thinned by uniform attack, releases concentrated acid, caustic, or solvent into the workplace. Beyond the immediate injury risk, a reportable spill triggers regulatory investigation, cleanup cost, and potential production suspension. Corrosion resistance is, in regulatory terms, a primary layer of protection.
Product Contamination
In electronics, pharmaceutical, and high-purity chemical service, corrosion products are contamination. Dissolved iron or nickel ions from a corroding metallic pump can ruin a batch of etchant or a reactor charge worth far more than the pump itself. Where product purity carries commercial value, corrosion resistance is a quality specification, and non-metallic wetted parts are the standard answer.
How Corrosion Resistance Is Engineered into a Chemical Pump
Corrosion resistance is achieved through deliberate choices in material, architecture, and sealing. Three engineering routes cover most industrial duties.
Fluoroplastic Lined Construction
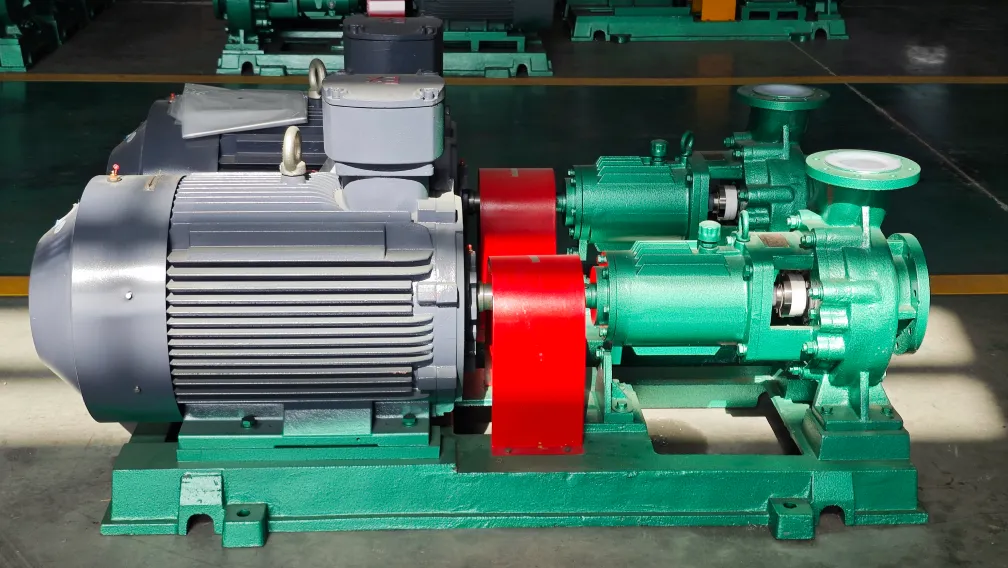
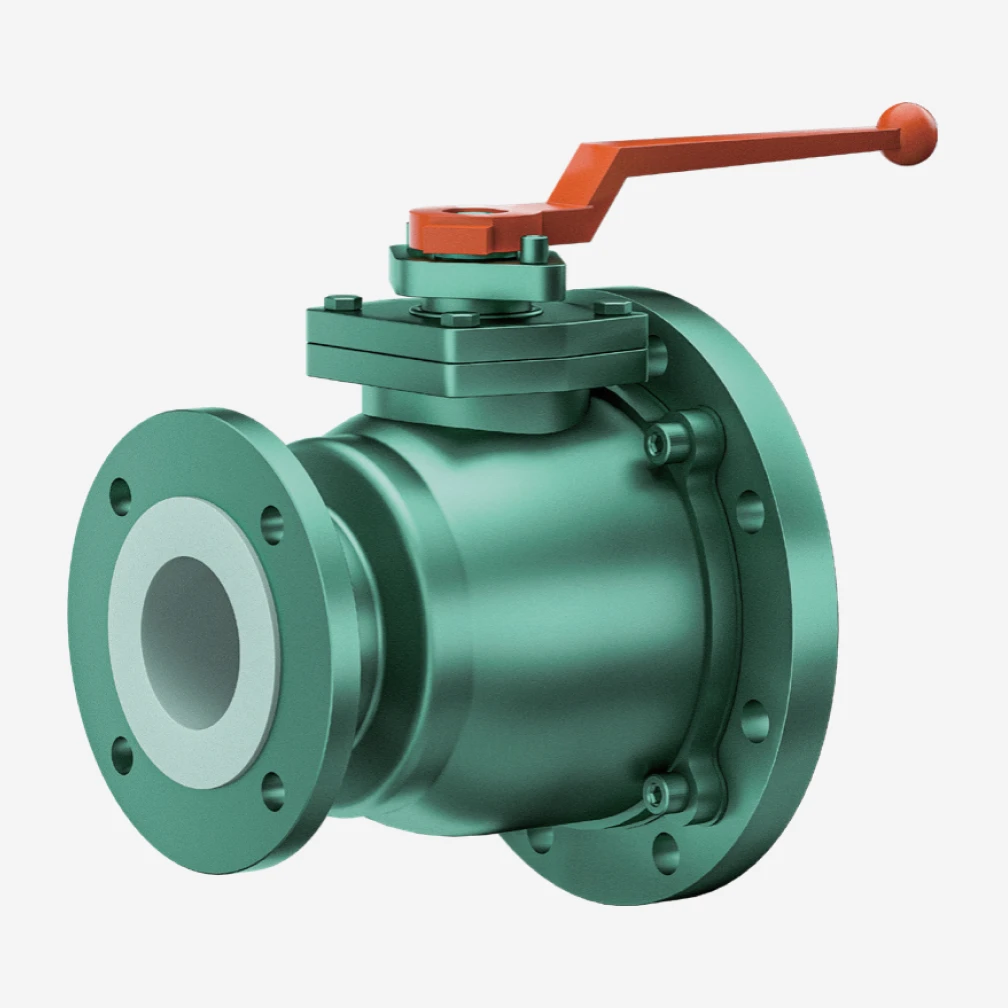
The most widely used route for strong acids, alkalis, and oxidizers: a ductile iron or steel pressure casing carries the mechanical load, while a molded lining of FEP, PFA, or fluoroplastic alloy, several millimeters thick, isolates every wetted surface from the fluid. Fluoroplastics resist virtually all industrial chemicals at any concentration at temperatures up to 150°C, and because the lining is non-metallic, galvanic couples and metal ion leaching disappear entirely. Industrial fluoroplastic lined centrifugal pumps built this way cover flows from 3 to 600 m³/h and heads to 80 m, which spans the bulk of acid transfer duties in chemical, metallurgical, and surface treatment plants.
Thick UHMWPE Linings for Corrosive Slurries
Where the fluid carries abrasive solids, a thin fluoroplastic lining can be scratched through. Ultra-high-molecular-weight polyethylene solves this: lined at 8 to 20 mm thickness over a steel casing, it combines broad acid and alkali resistance with abrasion resistance superior to hardened steel. The low-friction surface also resists scale adhesion in crystallizing duties. This construction is the standard for wet metallurgy, phosphate fertilizer, and flue gas desulfurization service.
Sealless Magnetic Drive Containment
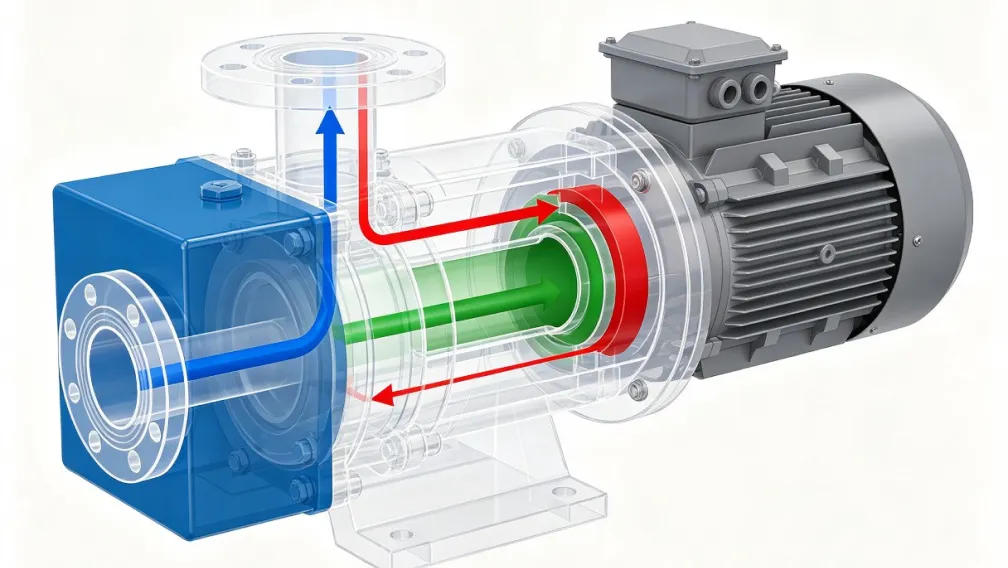
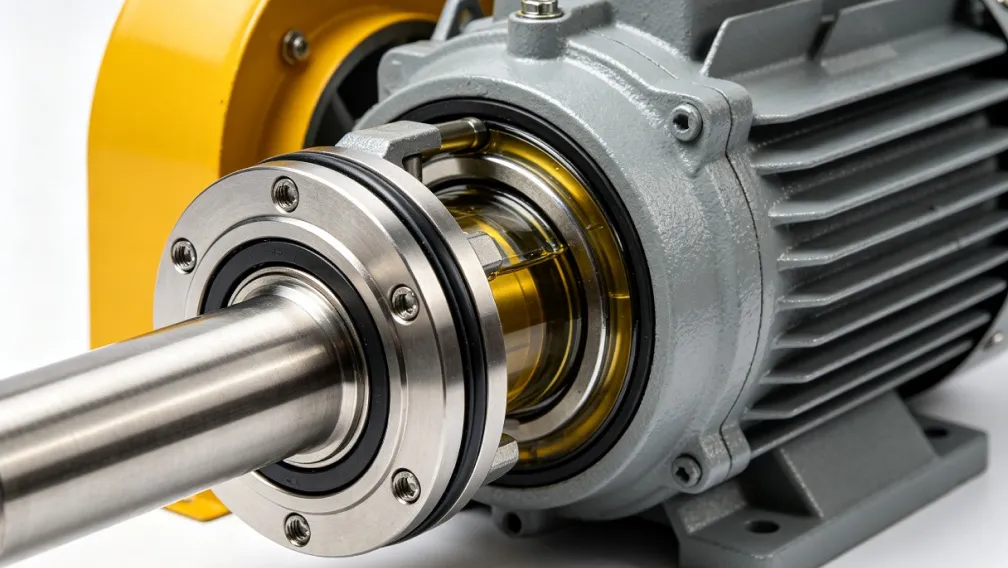
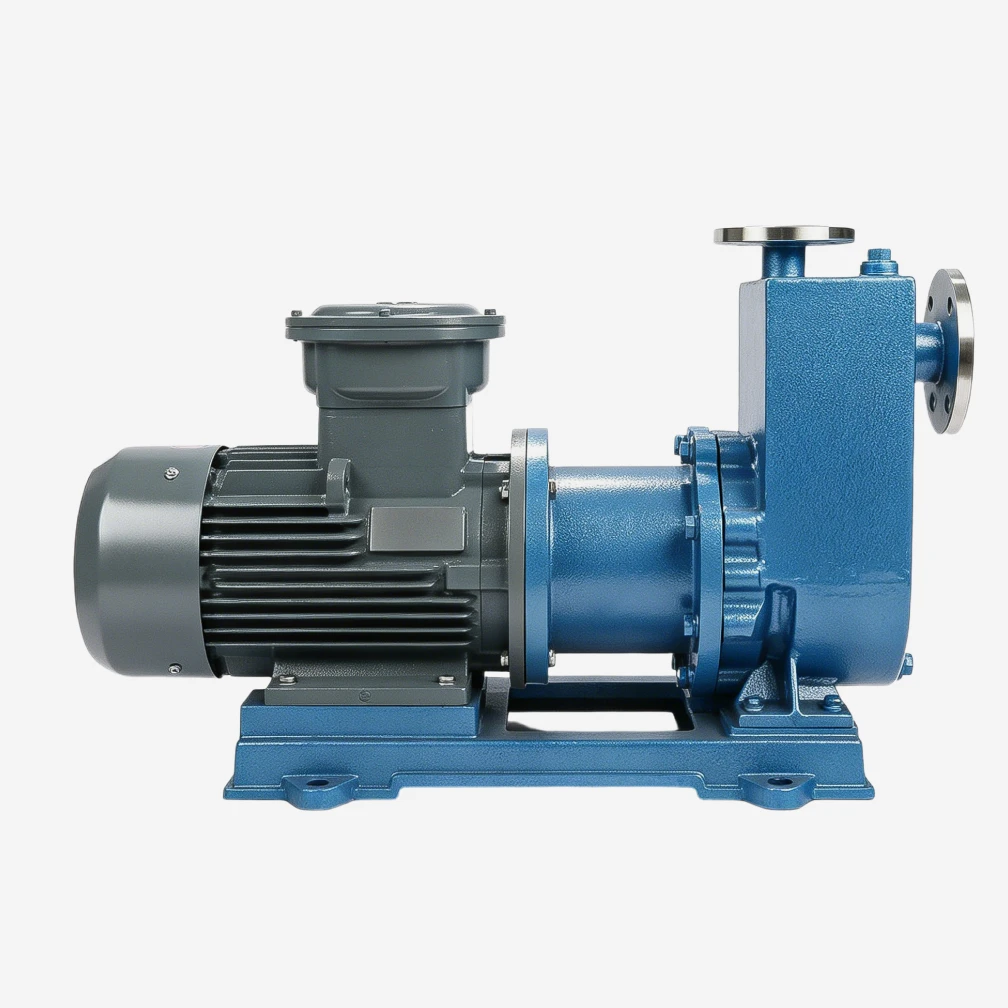
Corrosion resistance at the wetted surfaces solves only half the problem if the shaft seal still leaks. A mechanical seal is the most chemically stressed component in any pump: its faces, springs, and elastomers sit directly in the process fluid under pressure and motion. A sealless magnetic drive pump removes the shaft penetration completely. Torque passes through a stationary containment shell via magnetic coupling, the fluid stays hermetically sealed inside the casing, and the most failure-prone corrosion target in the machine simply ceases to exist. For toxic, volatile, flammable, or high-purity fluids, this architecture converts corrosion resistance into genuine zero-leakage containment.
Matching Corrosion Resistance to the Real Fluid
Corrosion resistance is always specific, never generic. A material that is excellent in one duty can fail quickly in another, and two variables change the answer most often:
- Concentration. Carbon steel stores 98% sulfuric acid safely at ambient temperature but corrodes rapidly in the same acid diluted to 60%. Stainless steel resists nitric acid yet fails in hydrochloric acid at almost any concentration.
- Temperature. Corrosion rates roughly double with every 10°C rise. A lining rated for a fluid at 40°C may not be suitable at 90°C, and temperature limits differ sharply between FEP, PFA, UHMWPE, and metallic alloys.
The practical rule is simple: material selection must start from the actual fluid name, concentration, and operating temperature, checked against a verified chemical resistance table. Guesswork in this step is the single most common cause of premature chemical pump failure.
Material Choices at a Glance
The table below maps the main corrosion-resistant constructions to their typical duties. It is a starting point for discussion, not a substitute for checking the specific fluid against a resistance table.
| Construction | Typical fluids | Temperature range | Typical duties |
|---|---|---|---|
| Fluoroplastic lined (FEP/PFA) | Strong acids, alkalis, oxidizers at any concentration | -20°C to 150°C | Acid transfer, pickling lines, chemical circulation |
| UHMWPE lined (8 to 20 mm) | Corrosive slurries with abrasive solids | -20°C to 90°C | Wet metallurgy, phosphate plants, FGD service |
| Fluoroplastic magnetic drive | Toxic, volatile, flammable, high-purity chemicals | -20°C to 100°C | Zero-leakage transfer, solvent handling, tank unloading |
| Stainless steel (304/316L) | Alkaline media, solvents, weak acids | Up to 120°C | Caustic transfer, general chemical service |
Conclusion
Corrosion resistance matters because in chemical service it determines everything that follows: uptime, energy consumption, safety compliance, product purity, and total cost of ownership. The mechanisms are understood, the engineering routes are proven, and the cost of getting it wrong is well documented. Specify the fluid precisely, choose the wetted material and sealing architecture to match, and the pump will return decades of uneventful service. YFTEL engineers corrosion-resistant pumping equipment across the full range of fluoroplastic lined, UHMWPE slurry, and magnetic drive designs. Send your fluid data, concentration, temperature, flow, and head, and we will return a verified material selection with the pump curve to match.
-

YFTEL Pumps
Fluid Engineers & Technical Support, YFTEL Pump
YFTEL is a chemical pump manufacturer based in Hangzhou, China, with a 26,000 m² production base in Hangzhou, China, with a 26,000 m² production base in Anhui. Using the CAS-patented Fluoroplastic Alloy material, we produce 300+ models of corrosion-resistant pumps, valves and piping, exported to 30+ countries.