
 English

The Seal Is the Highest-Wear Precision Component in the Pump
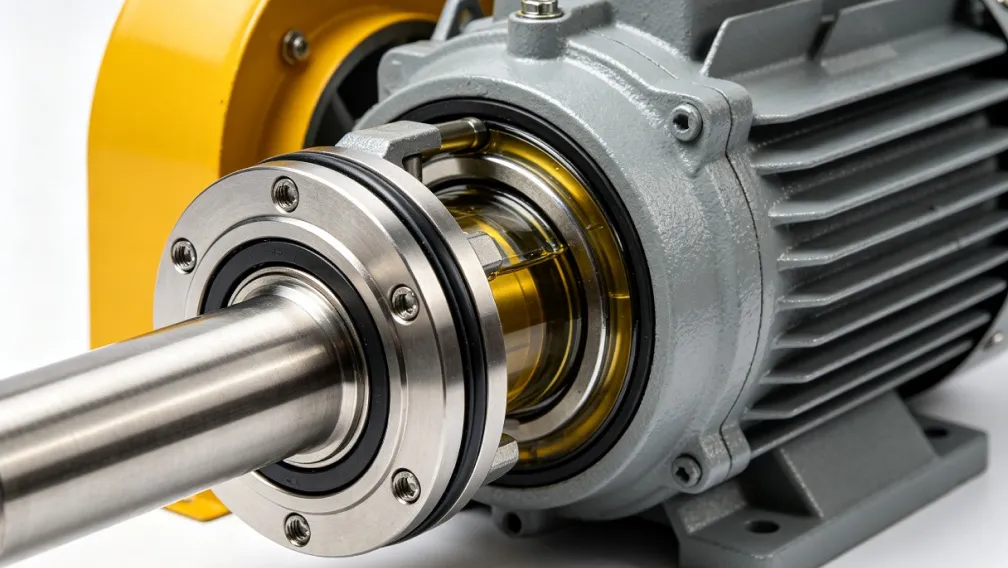
On a sealed chemical pump, no component works under harsher conditions than the mechanical seal. Its two lapped faces run against each other at shaft speed, inside the process fluid, under system pressure, separated by a liquid film measured in fractions of a micron. When the seal is healthy, leakage is a few milliliters per hour and invisible. When its supporting conditions degrade, the seal is the first component to announce the problem, usually as a rising leak that arrives weeks after the real cause. Mechanical seal maintenance is therefore mostly the maintenance of everything around the seal: the flush that feeds it, the barrier fluid that protects it, and the operating conditions that load it. This guide covers the four disciplines that determine seal life in corrosive service.
Flush Plans: The Seal's Life Support
What the Flush Does
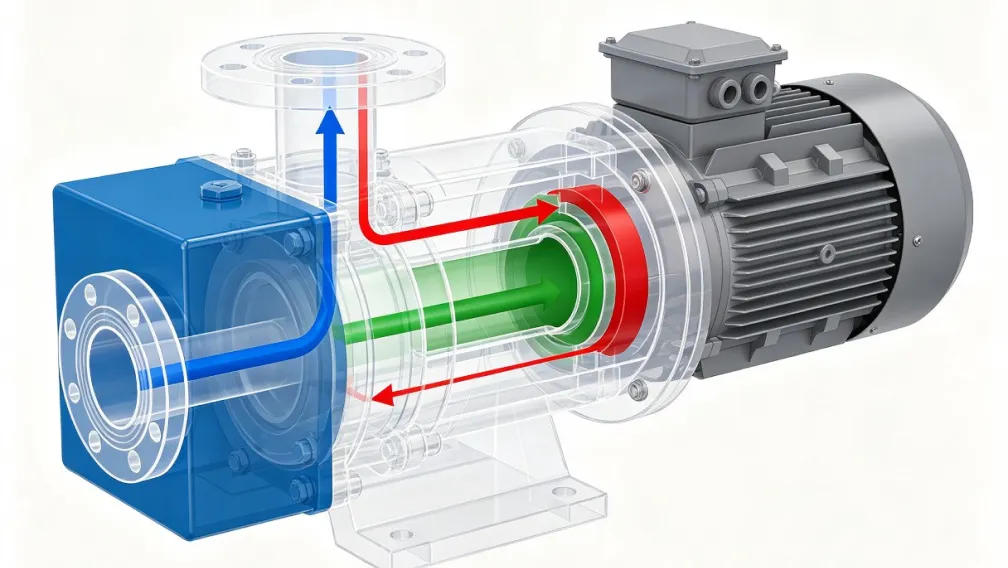
Every mechanical seal generates frictional heat at the faces and every process fluid carries risks: crystallization, solidification, dissolved solids, or simple chemical aggression toward the elastomers. A flush plan manages both. It circulates clean fluid through the seal chamber to carry heat away, keep the faces clean, and control the chemistry the seal actually sees. The most common arrangement on chemical pumps takes a clean stream from the pump discharge, runs it through a restriction into the seal chamber, and lets it return to the process. More demanding duties use an external clean fluid injected at controlled pressure. In both cases the principle is identical: the seal lives or dies by what flows past its faces, and the flush decides what that is.
The Blocked Flush: The Silent Seal Killer
The most destructive flush fault is also the least visible. A flush line that is connected but blocked shows normal gauges and a normal-looking pump, while the seal faces run dry and overheat. Crystallizing fluids such as caustic solutions and salt brines plug small flush ports progressively, so the blockage develops over weeks. Prevention is procedural: verify actual flush flow weekly, not just line pressure, because pressure can read correctly on a dead-headed line. On crystallizing services, include the flush orifice in the monthly inspection list and keep a cleaned spare orifice in stock.
Barrier Fluid Management for Double Seals
Where any process leakage is unacceptable, toxic, flammable, or aggressively corrosive fluids, the specification steps up to a double mechanical seal: two seal sets back to back with a pressurized barrier fluid between them. The barrier fluid is the working medium of the outer seal and the buffer for the inner one, and its maintenance is a discipline of its own.
- Pressure: keep barrier pressure above the seal chamber pressure at all times, typically by 1.5 to 2 bar. This sets the leak direction: any leakage is barrier fluid into the process, never process fluid outward. A barrier system that loses pressure inverts this logic and becomes a liability.
- Level: log the reservoir level daily. A falling level means barrier fluid is leaving somewhere, and on a healthy system it leaves through only one place: a seal face.
- Condition: sample the fluid monthly. Cloudy or discolored barrier fluid means process liquid has crossed the inner seal, which is now worn. Plan the face replacement on this evidence rather than on visible external leakage.
- Temperature: on hot duties, confirm the barrier cooler is functioning before summer peaks. Barrier fluid that overheats loses viscosity, the outer seal's fluid film thins, and face wear accelerates.
Seal Face Care and Replacement
Faces Are Consumables
Seal faces are engineered wear parts. Common pairings in chemical service run hard faces such as silicon carbide, alumina ceramic, or silicon nitride against a softer filled-PTFE or carbon face. The soft face sacrificially wears to maintain the seal, which is why faces are replaced as a set, stationary and rotating together: installing a new face against a worn one reproduces the worn geometry within days. For continuous-duty chemical pumps, annual face replacement on plan is the standard practice. On a rising leakage trend, replace at the first convenient outage rather than waiting for the calendar.
Handling Rules That Prevent Infant Mortality
A significant share of new seals fail within days, and the causes are almost always handling, not manufacture. Keep faces in their packaging until installation. Never touch the lapped face surface; fingerprint residue alone can disrupt the fluid film at startup. Use the correct installation sleeve or tool to pass the seal over shaft shoulders and keyways, because a chipped face edge is invisible until the leak starts. Verify the seal setting dimension against the drawing; an over-compressed seal wears in weeks, an under-compressed one leaks from the first rotation. And never attempt to lap a worn filled-PTFE face back into service: the filled material does not respond to lapping the way carbon does, and the result is a seal that leaks from startup.
Secondary Seals: The Overlooked Half
Attention naturally goes to the lapped faces, but roughly half of seal leaks in chemical service trace to the secondary seals: the O-rings and gaskets that close the static paths. Elastomers fail chemically long before they fail mechanically. A fluid that swells an O-ring by a few percent destroys its sealing force; one that hardens or cracks it opens a leak path that no face condition can compensate for. Every seal rebuild should start from an elastomer compatibility check against the actual process fluid and the flush or barrier fluid, both of which the secondary seals see continuously. Replace all elastomers at every face replacement; their cost is trivial against the labor of opening the seal chamber twice.
Operating Conditions: The Load Side of Seal Life
Seal life is set as much by how the pump is run as by how the seal is serviced. Three operating factors dominate. First, dry running: even brief operation without liquid destroys the face film and overheats the faces, which is why priming discipline is a seal maintenance issue. Second, operation far from the best efficiency point: a throttled or oversized pump runs with elevated vibration and shaft deflection, and the seal faces carry that motion directly. Third, solids in the fluid: abrasive particles that the flush cannot exclude score the faces rapidly. When a duty reliably contains solids that defeat the flush, the engineering answers are a slurry-duty seal design or a move to a sealless magnetic drive pump, which removes the dynamic seal from the problem entirely.
Reading the Leakage Trend
The leakage trend is the seal's own condition report, and learning to read it separates planned maintenance from emergency response. A new seal may show a brief initial weep that dries within hours as the faces run in; this is normal on many designs. The pattern that matters is a steady, measurable rise over weeks, which indicates progressive face wear or degradation of the secondary seals, and it is the trigger for planning replacement at the next outage. Sudden onset of heavy leakage is different again: it indicates an event such as dry running, a pressure spike, or face chipping, and it calls for immediate investigation rather than trend watching. Record leakage qualitatively but consistently, dry, occasional drip, steady drip, stream, in the daily log, so the trend survives shift changes.
Seal Maintenance Checklist
| Interval | Task |
|---|---|
| Daily | Observe and log leakage state; check barrier fluid level and pressure |
| Weekly | Verify actual flush flow; inspect flush lines for restriction |
| Monthly | Sample barrier fluid; review leakage trend; inspect flush orifice on crystallizing services |
| Quarterly | Review seal history against spares stock; verify barrier cooler function |
| Annual | Replace face set on continuous duty; inspect seal chamber, sleeve, and springs; verify setting dimensions |
Conclusion
Mechanical seal life in chemical service is built from four disciplines: a flush that verifiably flows, a barrier system that stays pressurized, clean, and cool, faces replaced as sets on evidence rather than on failure, and operating conditions that keep the pump near its design point. Managed this way, a seal in a lined centrifugal chemical pump delivers years of invisible, leak-free service; managed reactively, the same seal becomes a recurring release event. YFTEL supplies seal face sets, cartridge assemblies, and flush plan guidance for every sealed pump we build. Send us your fluid data, operating pattern, and current leakage history, and our engineers will review whether your seal arrangement and maintenance plan match the duty.
-

YFTEL Pumps
Fluid Engineers & Technical Support, YFTEL Pump
YFTEL is a chemical pump manufacturer based in Hangzhou, China, with a 26,000 m² production base in Hangzhou, China, with a 26,000 m² production base in Anhui. Using the CAS-patented Fluoroplastic Alloy material, we produce 300+ models of corrosion-resistant pumps, valves and piping, exported to 30+ countries.