
 English

Chloride Is the Defining Enemy of Stainless Pump Construction
More stainless steel pumps fail from chloride attack than from any other single cause, and the failures share a common trait: they arrive without warning. A pump handling seawater, brine, or a chloride-bearing process stream can look perfect from outside while pitting eats through its impeller from a handful of isolated points, and a chloride-stressed casing can crack under load with no visible precursor at all. Chloride service is therefore a selection problem first and a maintenance problem second. Understanding how chlorides defeat stainless steel, where the grade boundaries actually lie, and which upgrade path fits which duty is the difference between a pump that survives the service and one that becomes a case study.
How Chlorides Attack Stainless Steel
Pitting Corrosion
Stainless steel survives by its passive film, a chromium oxide layer a few atoms thick that reforms continuously in oxidizing conditions. Chloride ions break that film down locally, at inclusions and surface defects, and once the film is breached at a point, the chemistry at the breach becomes self-accelerating: the small anodic pit dissolves metal rapidly while the large surrounding cathode drives it. The result is a narrow, deep hole that can perforate a component while 99 percent of its surface remains untouched. Pitting is invisible to casual inspection and to most monitoring, which is what makes it dangerous: the first symptom is often the leak itself.
Crevice Corrosion
Any geometry that traps a stagnant micro-volume of fluid, gasket faces, O-ring seats, deposits, fastener threads, creates a crevice where oxygen is consumed and chloride concentrates. The crevice interior turns acidic and chloride-rich, and attack proceeds there even in fluids whose bulk chemistry the grade would tolerate. Pumps are full of crevices by design, which is why a grade that survives a flowing chloride stream may still fail at its own flanges and seal seats.
Stress Corrosion Cracking
The most sudden of the three mechanisms needs three ingredients together: a susceptible alloy, tensile stress, and a chloride-bearing environment above a threshold temperature. Standard austenitic grades, 304 and 316L, become vulnerable in chloride service above roughly 50 to 60°C, and the stress is always present, from pressure, assembly, and thermal expansion. Cracks propagate with little deformation and no visible warning, and failure is rapid when it comes. The practical rule that falls out of the mechanism: hot chloride service excludes standard austenitic grades regardless of how moderate the chloride level seems.
Where the Grade Boundaries Lie
Chloride limits are not single numbers; they move with temperature, pH, and crevices. As working guidance for clean pump service: 304 suits low-chloride, near-neutral water at ambient temperature and exits the discussion early. 316L, with its molybdenum content, extends the envelope to moderate chloride levels at ambient temperature, which is why it serves in many brackish and mildly saline duties, but it remains unsuitable for seawater at elevated temperature and fails the stress cracking threshold in hot chloride service. Seawater itself sits beyond both standard grades for anything but cool, clean, brief exposure. The boundaries tighten further wherever crevices exist and wherever the fluid is acidic, because low pH accelerates every chloride mechanism. Any duty near a boundary belongs to a documented verification, not an assumption.
Comparing Grades Quantitatively: The Pitting Resistance Equivalent
Engineers comparing chloride-resistant alloys use the pitting resistance equivalent number, PREN, calculated from each grade's chromium, molybdenum, and nitrogen content. The number compresses alloy chemistry into a single ranking of pitting resistance: 304 sits near the bottom of the usable range, 316L sits meaningfully higher because of its molybdenum, duplex 2205 rises well above 316L, and super duplex and nickel alloys extend the scale from there. As working orientation, PREN values around 40 mark the level generally associated with seawater service. The number is a screening tool rather than a guarantee, because crevices, temperature, and pH shift real-world performance around any single figure, but it prevents the most common grade-selection error: assuming that two stainless steels are interchangeable because both carry the name. In chloride service, the difference between grades is the difference between a pump that survives and one that pits.
The Upgrade Paths
Duplex Stainless Steels
Duplex grades such as 2205 combine austenitic and ferritic structures, and the combination attacks the chloride problem from two sides: the ferritic phase raises resistance to stress corrosion cracking dramatically, while the balanced chemistry lifts pitting resistance well above 316L. Duplex is the standard metallic answer for seawater, chloride brines, and produced water, and it keeps the full mechanical advantages of metal construction: high pressure capability, temperature headroom, and tolerance of solids and thermal cycling. Where the duty is hot, pressurized, or mechanically demanding and the chemistry is chloride-bearing but otherwise defined, duplex is usually the first upgrade considered.
Nickel Alloys
Where chloride combines with acidity, oxidizing power, or high temperature beyond duplex limits, nickel alloys such as the Hastelloy-type grades extend the envelope further. They handle hot chloride-acid mixtures that defeat every stainless grade, at a cost that reflects their alloy content. Their role in pump specification is targeted: they answer duties whose chemistry is severe but defined, where polymer temperature limits rule out linings.
The Non-Metallic Route
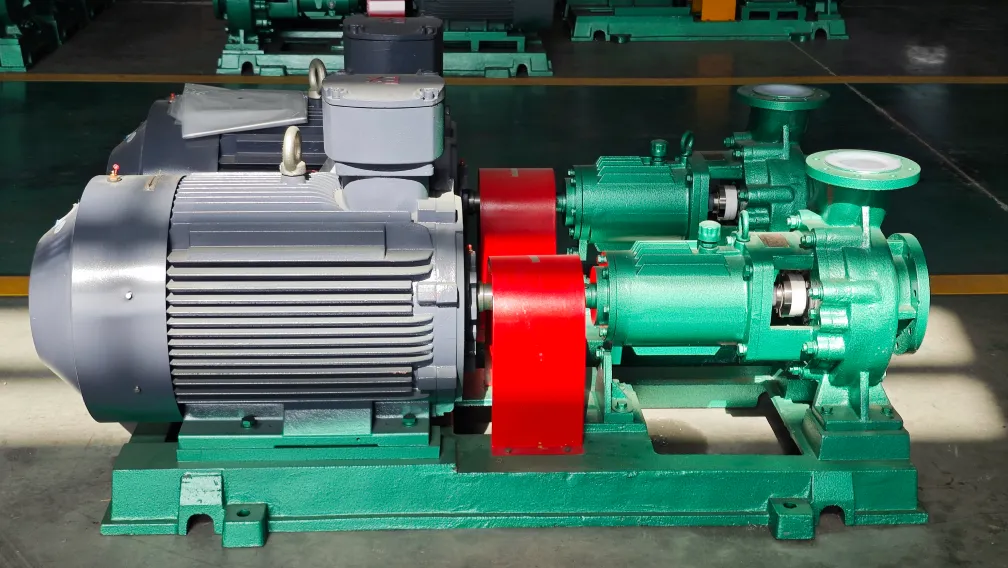
Fluoroplastic-lined pumps sidestep the chloride problem entirely. FEP, PFA, and PTFE carry no passive film, pit no pits, and crack no cracks: chloride chemistry is simply irrelevant to them. For chloride service within their temperature range, roughly to 150°C and beyond in PFA constructions, lined pumps deliver total chloride immunity at a fraction of high-alloy cost. This is why seawater intake, brine transfer, and ferric chloride dosing in water treatment default to lined construction, and why a fluoroplastic magnetic drive pump covers hazardous chloride fluids with zero leakage as well. UHMWPE extends the same immunity to chloride slurries, where solids accompany the chemistry.
Selection Logic for Chloride Duties
The working sequence runs on three questions. First, define the chloride condition fully: concentration, temperature, pH, and whether crevices and solids are part of the picture, because each one tightens the grade boundaries. Second, test the metallic path: cool, dilute, neutral chloride service may suit 316L; seawater and brines point to duplex; hot acidic chlorides point to nickel alloys. Third, test the polymer path: within temperature limits, fluoroplastic lining removes the chloride variable altogether and usually at lower cost than the alloy that would survive it, with UHMWPE covering chloride slurries. The decision between the alloy answer and the polymer answer then falls to temperature, pressure, solids, and mechanical duty, the factors chloride does not decide.
Duty-to-Material Summary
| Chloride duty | Recommended material route |
|---|---|
| Low-chloride water, ambient, neutral | 304 or 316L |
| Brackish water, moderate chloride, ambient | 316L, verified against crevice conditions |
| Seawater intake and transfer | Duplex 2205 or fluoroplastic lined |
| Hot chloride service above 50 to 60°C | Duplex or alloy; standard austenitic excluded |
| Ferric chloride and acidic chlorides | Fluoroplastic lined; nickel alloy where temperature demands |
| Chloride slurries with solids | UHMWPE slurry construction |
| Hazardous volatile chloride fluids | Fluoroplastic magnetic drive |
Operating Discipline in Chloride Service
Material selection closes most of the chloride risk, and operating discipline closes the rest. Chloride pumps benefit from three practices beyond the standard maintenance schedule. Avoid stagnant conditions: chloride attack concentrates wherever fluid stands, so idle pumps on chloride duty should be drained and flushed with fresh water rather than left loaded. Inspect crevices at every opening: gasket faces, seal seats, and fastener threads are where crevice corrosion starts, and they deserve the same systematic attention as the wetted surfaces. And treat deposits as attack sites: sediment and scale create artificial crevices, so strainers, low points, and dead legs in chloride systems earn regular cleaning. These practices cost little and address the exact geometries where chloride mechanisms begin.
Conclusion
Chloride service punishes assumptions. Pitting perforates without visible warning, crevices attack where bulk chemistry looks safe, and stress corrosion cracking excludes standard stainless grades from hot chloride duty outright. The upgrade paths are proven: duplex for metallic seawater and brine service, nickel alloys for hot acidic chlorides, and fluoroplastic linings for full chloride immunity within polymer temperature limits. The selection runs on complete duty data, chloride level, temperature, pH, crevices, and solids, verified before the pump is built. YFTEL manufactures chloride-duty pumps across duplex stainless and the full fluoroplastic-lined range, including lined centrifugal chemical pumps for seawater and brine transfer. Send us your chloride analysis and operating window, and our engineers will return a material route with the boundary logic documented.
-

YFTEL Pumps
Fluid Engineers & Technical Support, YFTEL Pump
YFTEL is a chemical pump manufacturer based in Hangzhou, China, with a 26,000 m² production base in Hangzhou, China, with a 26,000 m² production base in Anhui. Using the CAS-patented Fluoroplastic Alloy material, we produce 300+ models of corrosion-resistant pumps, valves and piping, exported to 30+ countries.