
 English

The Lining Is the Pressure Boundary's Bodyguard
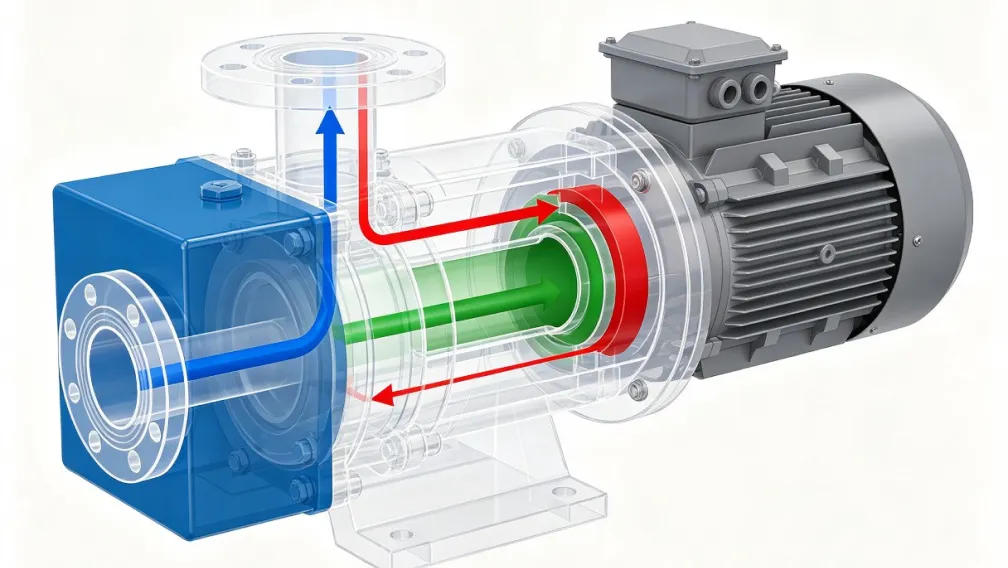
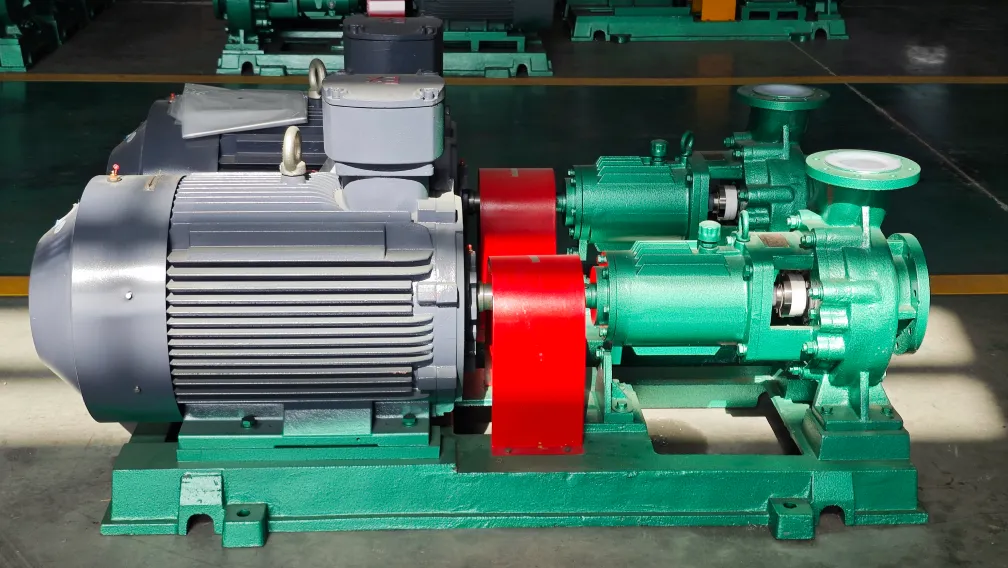
In a lined chemical pump, the metal casing carries the pressure and the lining carries the chemistry. This division of labor is what makes the construction economical: ductile iron or steel provides strength at a fraction of alloy cost, while a few millimeters of fluoroplastic, or a thicker layer of UHMWPE, keeps the process fluid from ever touching it. The arrangement works only while the lining is intact. A pinhole that reaches the metal underneath converts a corrosion-proof pump into a corroding one, and the attack then proceeds unseen between lining and casing until the pressure boundary itself is compromised. Lining inspection exists to find damage at the stage where it is a relining job rather than a casing replacement, and this guide covers how to inspect, what to look for, and how to decide between continued service, relining, and replacement.
How Linings Fail
Lining damage follows a small set of mechanisms, and knowing them directs the inspection to the right places. Mechanical wear concentrates where velocity and turbulence peak: the volute cutwater, the impeller eye and vane edges, and any restriction in the flow path. Thermal damage comes from local heat, dry running being the common cause, which blisters and distorts the lining where it contacts hot components. Chemical permeation is slower: some fluids diffuse into fluoroplastics over years and attack the adhesive interface or the metal behind, showing first as discolouration or blistering. Mechanical abuse completes the list: over-torqued or misaligned flanges crush the lining turnout on flange faces, and impact during maintenance chips edges. Welding or flame work near a lined pump deserves its own warning: local heat destroys the lining from the inside, and the damage is often invisible until the lining separates.
Inspection Planning: Where and When
Lining inspection is an outage activity, so it must be planned around the shutdown calendar. The full survey belongs in the annual overhaul; pumps in severe service, high velocity, solids, or thermal cycling, justify a half-yearly check of the known hot spots. Prepare before opening the pump: isolate, drain, and flush or neutralize the wetted end per the fluid's safety data, and have the previous inspection records at hand so changes since last time are visible rather than guessed. On magnetic drive pumps, the containment shell inspection and the lining inspection happen in the same opening, since both are wetted-surface checks.
Safety Preparation Before Opening a Lined Pump
The fluids that justify lined construction are the same fluids that make opening one hazardous. Before any inspection, isolate the pump electrically and mechanically, close and lock the suction and discharge valves, and drain the casing through the drain connection into the containment system rather than onto the floor. Flush or neutralize the wetted end according to the fluid's safety data sheet; acid residues trapped in lining cracks and flange recesses survive draining and contact skin during disassembly. Treat every lined pump as chemically loaded until the flush water runs neutral and the atmosphere around the opening is confirmed safe. Only then does inspection begin.
Inspecting Fluoroplastic Linings
Visual and Tactile Survey
Fluoroplastic linings, FEP, PFA, PTFE, and fluoroplastic alloys, announce most defects visually. Work systematically over the casing bore, cover, and impeller, with attention weighted to the high-velocity zones. Look for discolouration, which records thermal events or permeation; blistering, which indicates the lining has separated from the metal behind it; cracking, usually at stress concentrators such as corners and transitions; pinholes, the critical finding, because each one is a direct path to the metal; and local thinning, which predicts the pinholes of next year. A flashlight held at a low angle makes blisters and thinning shadows visible that direct lighting hides. Run a fingertip over suspect areas: blisters feel hollow, and thinned areas feel different from the surrounding surface.
Flange Face Turnouts
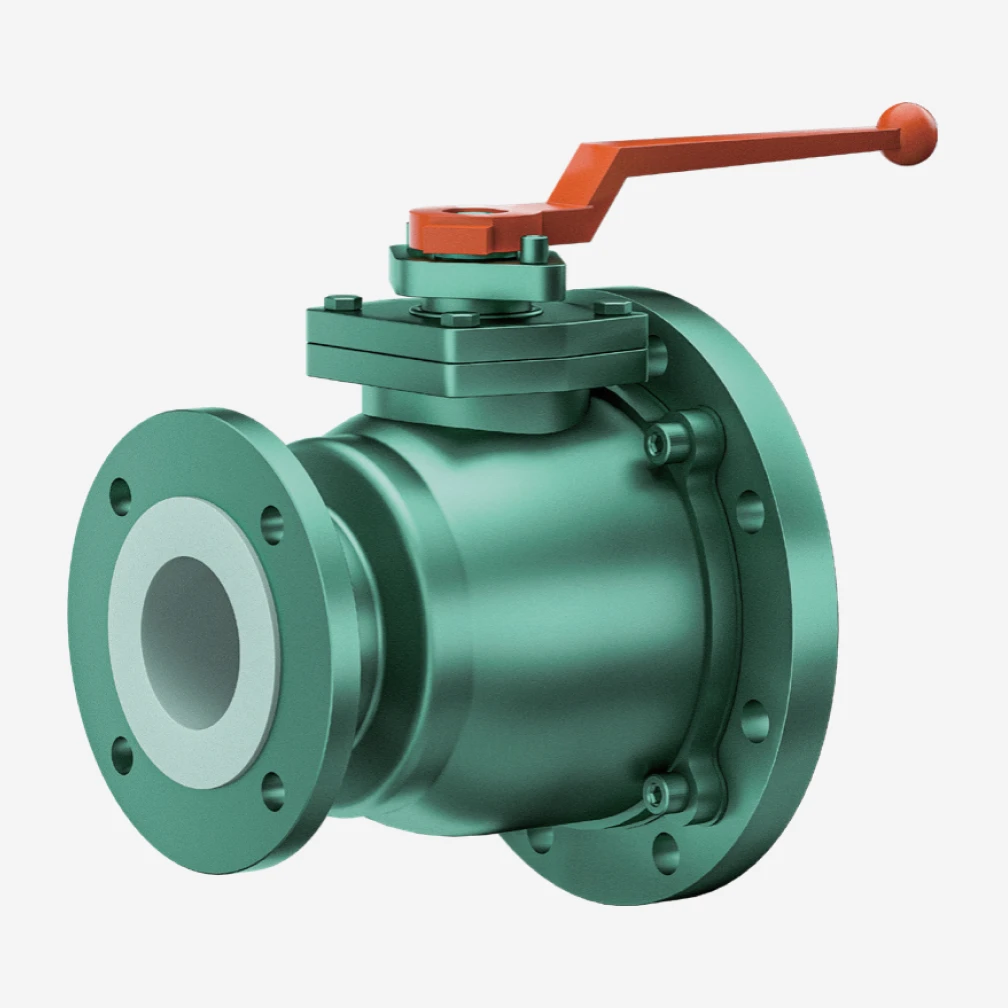
The lining turnout, the section folded over the flange face to form the sealing surface, is the most common leak path on lined pumps, valves, and piping. Inspect it at every opening for crushing, cracking, and scoring. The causes are almost always assembly faults: flanges over-torqued, misaligned, or forced together under pipe strain. Correct torque with a cross pattern protects the turnout; so does the discipline of never drawing misaligned flanges together with bolts.
Thickness Measurement
Where the design permits access, gauge lining thickness at the high-wear zones and record the values against the original specification. The numbers matter less individually than as a series: a lining losing a measurable fraction of its thickness per year has a calculable relining date, and that date belongs in the maintenance plan rather than in a breakdown report.
Inspecting UHMWPE Slurry Linings
The UHMWPE lining in a slurry pump differs from fluoroplastic in one fundamental way: it is designed to wear. At 8 to 20 mm thick, the lining is a sacrificial wear component with a planned consumption rate, and inspection is measurement rather than defect hunting. Gauge residual thickness at the defined wear zones, the volute, the impeller shroud, and the suction-side liner, record the trend, and project the wear forward. Plan relining when residual thickness approaches the manufacturer's minimum, commonly around half the original layer, and well before the steel housing is approached. The failure mode being prevented is specific: once slurry reaches the steel, erosion-corrosion of the housing proceeds far faster than the lining ever wore, and the repair scope jumps from a lining job to a casing replacement.
The Decision: Run, Reline, or Replace
Inspection findings resolve into three dispositions. Continue in service when the survey shows no pinholes, no exposed metal, blisters absent or small and stable, and thickness trend comfortably above minimum; record everything and return the pump to duty. Reline when pinholes, cracking, or exposed metal are found but the metal housing remains sound: relining restores the full corrosion barrier at a fraction of new-pump cost, which is one of the structural economic advantages of lined construction. Replace the component when the metal behind the lining is itself attacked, when the casing shows pressure-boundary damage, or when repeated relining becomes uneconomic. One rule overrides all judgment calls: any pinhole means the metal is exposed, and a pump with exposed metal in corrosive service goes onto the relining plan before it returns to service, not after the next campaign.
Extending Lining Life
Most lining life is determined before the inspection ever happens, by how the pump is operated. Keep the pump near its best efficiency point, because off-design operation raises the velocities and turbulence that wear linings fastest. Prevent dry running without exception, since the thermal damage it causes to linings arrives in the same seconds that destroy seals and bearings. On lined systems as a whole, keep flange standards matched (PN10/PN16 or ANSI 150 end to end) so turnouts align and torque distributes evenly. And handle lined components correctly outside the pump: store spare lined casings, impellers, and piping flat, out of direct sunlight and away from heat, because polymer linings distort and age in storage just as they do in service.
Inspection Record Template
| Record item | Content |
|---|---|
| Component and location | Casing bore, cover, impeller, cutwater, flange turnouts, containment shell |
| Visual findings | Discolouration, blistering, cracking, pinholes, scoring: location and extent |
| Thickness readings | Measured values at defined points vs original specification and previous survey |
| Wear rate | Thickness loss since last survey, projected relining date |
| Disposition | Continue, reline, or replace, with justification |
| Corrective actions | Operating or assembly faults found: flange torque, alignment, duty point |
Conclusion
Lining inspection is the maintenance discipline unique to lined pump construction, and it is what turns the lining's sacrificial role into an economic advantage: wear is measured, relining is planned, and the metal pressure boundary is never exposed to the fluid. The practice is straightforward: survey visually at every opening, gauge thickness at the wear zones, protect flange turnouts during assembly, and treat any pinhole as a relining trigger. YFTEL supplies relining services and lined spare components for the full range of fluoroplastic and UHMWPE centrifugal chemical pumps and magnetic drive pumps. Send us your inspection records and wear measurements, and our engineers will help you project relining dates and stock the right lined spares.
-

YFTEL Pumps
Fluid Engineers & Technical Support, YFTEL Pump
YFTEL is a chemical pump manufacturer based in Hangzhou, China, with a 26,000 m² production base in Hangzhou, China, with a 26,000 m² production base in Anhui. Using the CAS-patented Fluoroplastic Alloy material, we produce 300+ models of corrosion-resistant pumps, valves and piping, exported to 30+ countries.